Though excipients do not carry the medicinal benefit of the drug, they can make a big impact on the manufacturing, storage, release, and performance of the drug.
This is why the selection process of the excipient is not easy; it is not just about finding the excipient at the right price.
The buyer could have found a supplier of the excipient that provides the needed quality at the right price. But the first question to ask would be: Who made the excipient? Is the grade appropriate for pharmaceutical use? Can the supplier provide reliable batch documentation? Are the manufacturing and distribution controls adequate?
The U.S. FDA has specifically advised buyers to know their bulk drug substance and excipient suppliers and understand how those suppliers establish the quality of the materials they provide.
Here are the practical guidelines buyers need to adhere to.
1. Ensure That the Excipient is Suitable for Its Proposed Purpose
One of the first mistakes buyers can make is assuming that a material described as "pharma grade" is automatically suitable for every pharmaceutical application.
The intended use matters.
Before evaluating a supplier, define exactly what you need:
- Excipient name and grade
- Intended dosage form
- Route of administration
- Required quality specifications
- Applicable pharmacopoeial standards
- Functional requirements
- Packaging requirements
The excipient can have a certain function within a formulation, being used as a binder, filler, lubricant, preservative, disintegrator, or release controlling agent.
Its physicochemical properties can thus influence the final product.
Based on FDA standards, the physicochemical characteristics of the excipient may influence the efficiency, stability, bioavailability, and processibility of the drug product.
The first question that is not supposed to be asked is hence, "Who has the lowest price?"
It should be, "Is this exact material appropriate for our application?"
2. Identify the Actual Manufacturer
This is one of the most important checks—and one that is easy to overlook when purchasing through distributors.
A supplier may be:
- The original manufacturer
- An authorized distributor
- A trader
- A repacker
- An importer
- An agent
These roles are not interchangeable.
Buyers should know who actually manufactured the excipient and where that manufacturing took place.
It is particularly relevant when looking into a quality problem or tracking a lot.
FDA has highlighted the importance of supply chain transparency as well as the original manufacturer identification in case of repackaging of the product.
Prior to selecting any supplier, you have to ask yourself the following questions:
- Who manufactured this material?
- Where was it manufactured?
- Has there been any reconditioning or relabeling?
- Is it possible to trace the production batch to its original manufacturer?
Inability to provide clear answers to these questions warrants further investigation of the supplier.
3. Evaluate the Supplier's Quality System
A supplier's website and product catalogue tell you very little about how consistently it controls manufacturing.
Procurement and quality teams should therefore evaluate the supplier's quality system.
Depending on the material and intended use, this may include reviewing:
- GMP controls
- Quality-management systems
- Manufacturing procedures
- Quality-control testing
- Deviation management
- CAPA processes
- Change control
- Complaint handling
- Audit history
The International Pharmaceutical Excipients Council (IPEC) identifies supplier qualification, auditing, quality agreements, risk assessment, CoAs, and change management as important areas of excipient quality practice.
The key point is that a certificate alone should not replace supplier assessment.
A certificate tells you something about a supplier's stated compliance status. A qualification process examines whether the supplier can consistently deliver material that meets your requirements.
4. Don't Treat the Certificate of Analysis as a Checkbox
It is an important aspect when procuring pharmaceutical raw materials; however, a buyer must think beyond asking, “Do you have a CoA?”
A better question to ask would be:
Does the CoA provide the information we need for this specific batch and material?
Review relevant information such as:
- Product identity
- Batch number
- Test results
- Specification limits
- Test methods
- Manufacturing information
- Date information
- Retest or expiry information, where applicable
IPEC's revised 2024 CoA guide was developed to support appropriate preparation and use of certificates of analysis for pharmaceutical excipients and to clarify responsibilities between excipient manufacturers and distributors.
A generic product specification and a batch-specific CoA serve different purposes.
For critical materials, that distinction matters.
5. Compare the Supplier's Specifications Against Yours
A related common error is not comparing the specifications of the supplier against your own.
Rather, buyers should conduct a comparison as follows:
Supplier specification → applicable standard → internal specification → intended application
Depending on the excipient, relevant attributes may include:
- Identity
- Assay or purity
- Water content
- Particle characteristics
- Microbial limits
- Residual solvents
- Elemental impurities
- Physical characteristics
- Other product-specific quality attributes
There is no universal checklist that applies identically to every excipient.
The appropriate tests and acceptance criteria depend on the material and its pharmaceutical application.
That is why procurement teams should involve quality and technical functions before approving a new source.
6. Assess Contamination and Cross-Contamination Risk
This is another area that can easily disappear during a price-focused procurement exercise.
Buyers should consider the possibility of contamination during:
- Manufacturing
- Processing
- Packaging
- Storage
- Repacking
- Transportation
The risk profile depends on the material and its supply chain.
This is particularly important for materials where contamination with potentially harmful substances could have serious consequences.
FDA has issued warnings related to quality problems involving bulk drug substances and excipients and has stressed the importance of knowing how suppliers test and control the quality of components used in medicines.
A supplier's ability to explain its contamination controls should therefore form part of the qualification process.
7. Check Storage and Transportation Conditions
Even a well-manufactured excipient can be compromised if it is improperly stored or transported.
Ask the supplier about:
- Recommended storage temperature
- Humidity requirements
- Light sensitivity
- Packaging configuration
- Warehouse conditions
- Transportation controls
- Handling procedures
This becomes especially important for materials with specific stability requirements.
IPEC's 2026 stability guidance work emphasizes establishing stability programs and substantiating appropriate storage conditions and shelf-life or retest claims for pharmaceutical excipients.
In other words, don't stop your assessment at the manufacturing site.
Consider what happens to the material between the factory and your warehouse.
8. Understand Change-Control Procedures
Supplier qualification is not a one-time event.
A supplier may change:
- Manufacturing location
- Manufacturing process
- Raw-material source
- Testing method
- Specifications
- Packaging
- Sub-suppliers
Any significant change could potentially affect the material.
Ask potential suppliers how they notify customers about relevant changes.
A documented change-control and notification process gives buyers greater visibility and allows quality teams to assess whether a change requires additional testing, qualification, or regulatory action.
This is one reason supplier relationships should be actively monitored rather than reviewed only when the next purchase order is issued.
9. Evaluate Supply Continuity Alongside Quality
Quality is critical, but supply continuity matters too.
Imagine that an excipient meets every specification but the supplier regularly misses delivery dates or cannot support your required volume.
That is still a procurement risk.
When evaluating pharma raw material suppliers, consider:
- Manufacturing capacity
- Lead time
- Minimum order quantity
- Production scalability
- Historical delivery performance
- Geographic concentration
- Backup production arrangements
- Communication responsiveness
For critical materials, having an alternative qualified source can provide valuable protection against unexpected disruptions.
10. Don't Confuse Excipient Suppliers With API Suppliers
Excipients and APIs are both important pharmaceutical raw materials, but they are not the same thing.
An API provides the pharmacological activity of a medicine, while an excipient serves another function within the formulation or manufacturing process.
This distinction matters during supplier qualification.
The sourcing strategies that can be used by the procurement team while looking for the suppliers of API or suppliers of raw material for API would remain almost similar but will not be exactly the same.
The same applies when looking for API and Pharma Raw Material Suppliers in world.
A large supplier network is useful, but every material and source still needs to be evaluated according to its specific risk and intended application.
The Excipient Supplier Compliance Checklist
Before approving a new excipient supplier, buyers should be able to answer these questions:
- Is the exact excipient grade suitable for our application?
- Who is the original manufacturer?
- Where is the manufacturing site?
- Is the supplier a manufacturer, distributor, or repacker?
- Can the supplier provide appropriate batch-specific CoAs?
- Do the specifications meet our requirements?
- Are appropriate quality and GMP controls in place?
- Are contamination risks adequately controlled?
- Are storage and transportation conditions suitable?
- Is batch traceability maintained?
- Does the supplier have a documented change-notification process?
- Is the supplier capable of delivering the amount required by us on time?
If there are many such questions that have not been answered, the supplier is probably not ready to be approved.
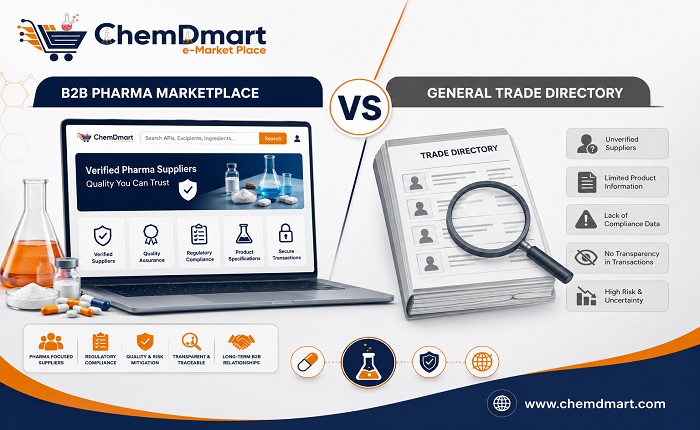
How a Pharma Raw Material Marketplace Can Help
The task of finding appropriate suppliers is often tedious and especially when procurement departments have to procure many materials or find substitutes.
A dedicated platform for pharmaceutical raw materials can make this task easier as it facilitates a buyer-supplier meeting ground through a B2B portal.
For procurement teams, this can make it easier to:
- Discover potential suppliers
- Explore alternative sources
- Submit RFQs
- Compare supplier responses
- Expand international sourcing options
- Search for API raw material suppliers
- Find API suppliers
- Explore broader pharmaceutical raw materials
However, there is an important distinction:
Supplier discovery is not supplier approval
A marketplace can help you find potential sources, but your procurement, quality, technical, and regulatory teams still need to perform the necessary due diligence.
How ChemDmart Supports Pharmaceutical Sourcing
ChemDmart is an example of a business-to-business marketplace that is designed for supplier identification, RFQ management, procurement intelligence, lead generation, and global sourcing.
In case a company needs to identify potential suppliers of pharma raw materials, the marketplace can be used to create an environment where such sourcing activities could take place.
It will enable buyers to conduct sourcing activities through ChemDmart for pharmaceutical and chemical materials, as well as for APIs and other pharma raw materials.
The value is not simply in finding another supplier.
It is in giving procurement teams greater visibility into the available sourcing landscape so they can make better-informed qualification and purchasing decisions.
The Bottom Line
Excipient sourcing should never be reduced to finding a product at the lowest possible price.
However, the main problem lies in determining the source that will provide the required substance in a consistent manner, both in terms of quantity, quality, and documentation.
Such routine steps as identification of the originator, review of the batch documents, contamination risk evaluation, change control, and storage conditions may acquire an extreme significance if something goes wrong.